Heavy Drop Forging & Press Shop
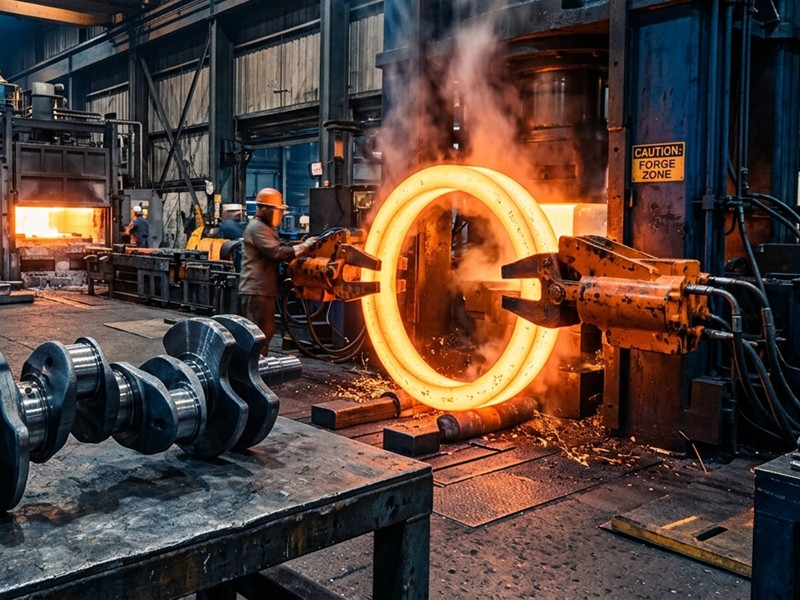
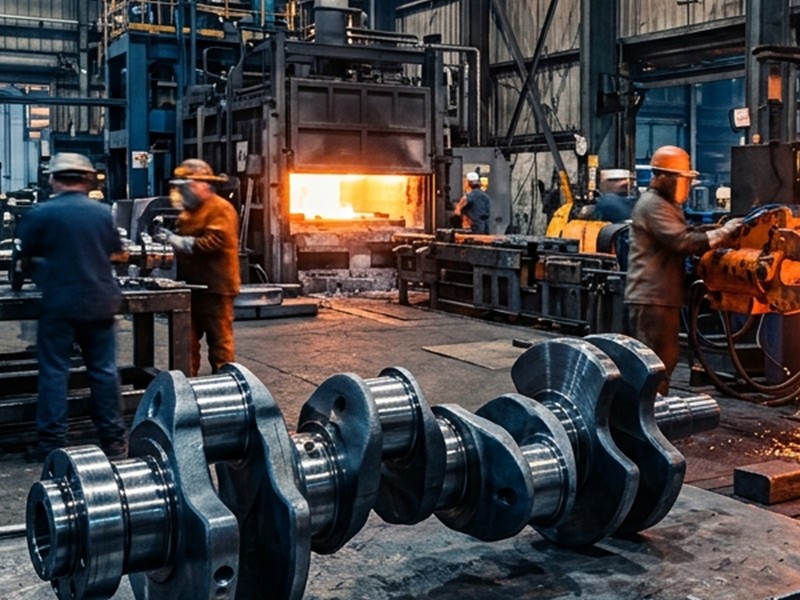
Heavy-duty pneumatic drop forging hammers, friction screw presses, and automated induction billet heating systems with continuous pyrometer optical temperature monitors.
State-of-the-art heavy drop forge hammers, automated continuous induction billet heaters, multi-axis CNC machining bays, calibrated heat treatment furnaces, and in-house metallurgical testing labs.
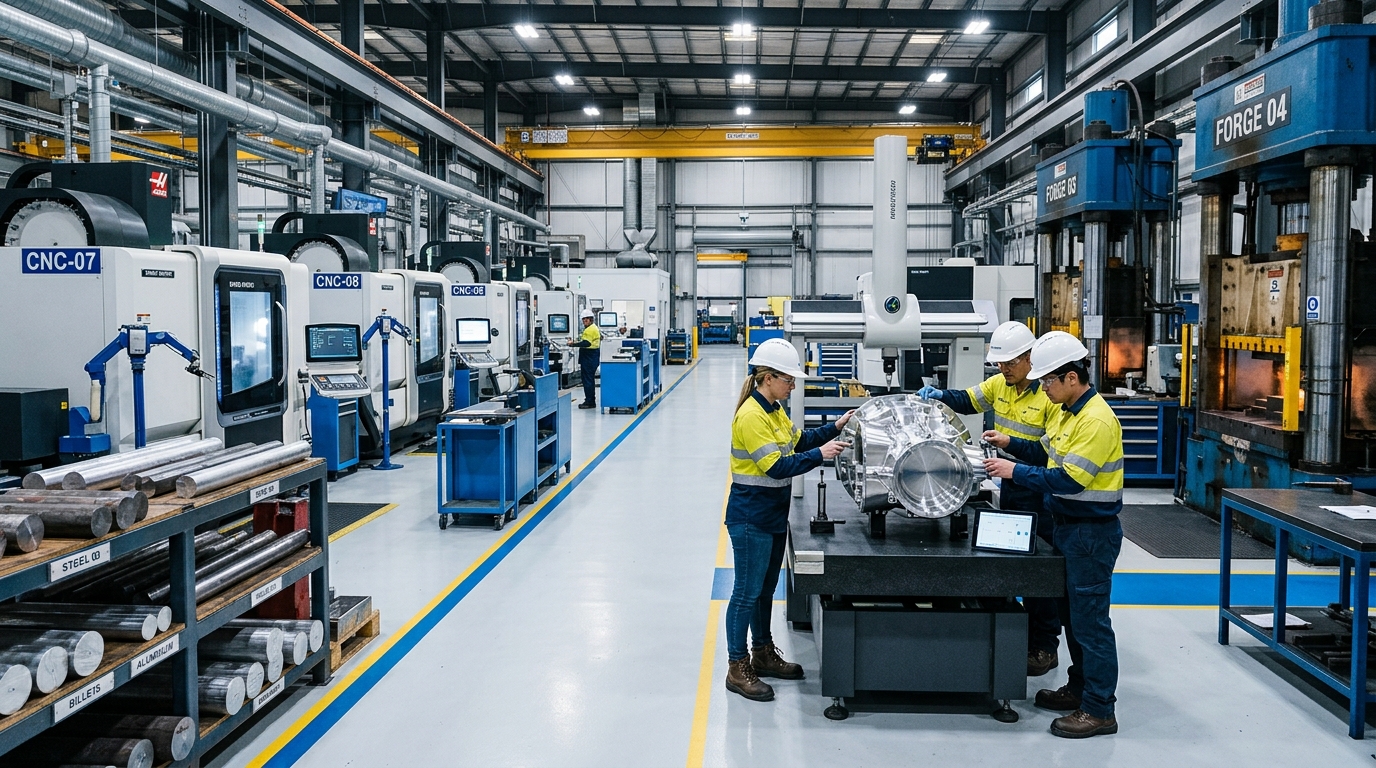
The Ankita Forge Industries manufacturing facility in Maharashtra, India is engineered for optimal metallurgical integrity, lean process flow, and high-volume precision output. Covering raw material cutting, induction heating, closed-die forging, automated heat treatment, CNC threading, surface finishing, and quality inspection under one roof, we eliminate third-party reliance and guarantee tight dimensional tolerances.
Equipped with overhead EOT cranes, continuous temperature-controlled pyrometer furnaces, and high-speed CNC lathes, AFI fulfills critical high-pressure piping orders for refineries, petrochemical skids, offshore platforms, and nuclear power projects worldwide.
Dedicated operational departments executing high-precision forging, machining, heat treatment, and quality inspection.
Heavy-duty pneumatic drop forging hammers, friction screw presses, and automated induction billet heating systems with continuous pyrometer optical temperature monitors.
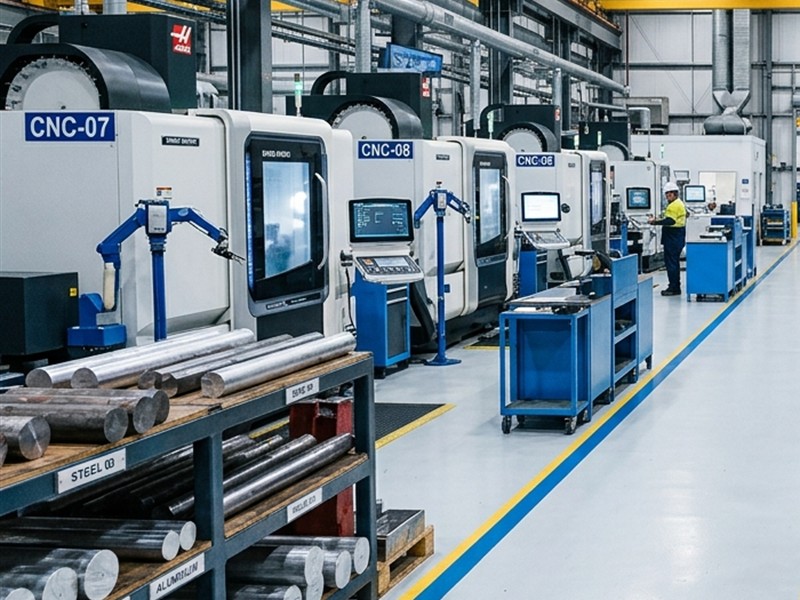
High-speed multi-axis CNC turning centers, vertical machining centers (VMC), and automated single-point thread cutting lathes producing mirror-smooth socket lands and threads.
Gas-fired furnaces with multi-channel digital PID temperature recorders executing Normalizing, Full Annealing, Quench & Tempering (Q&T), and Solution Annealing.
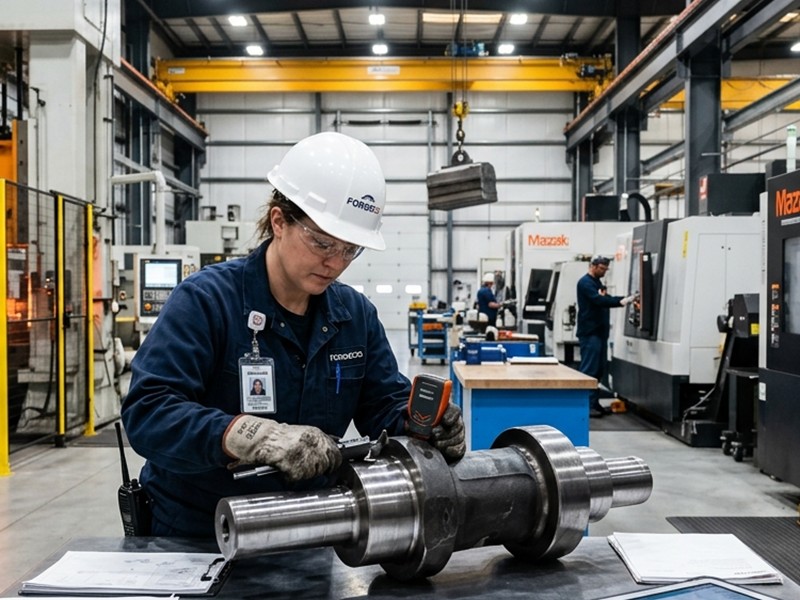
32-channel Optical Emission Spectrometer (OES), computerized Universal Testing Machine (UTM), sub-zero Charpy Impact Tester, and NDT ultrasonic inspection stations.
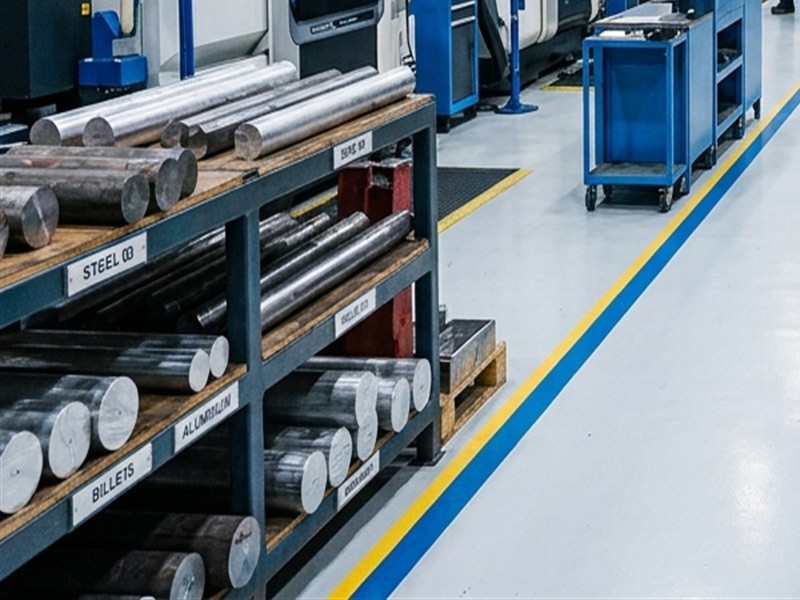
Extensive inventory of prime-grade certified round steel billets sourced from premier primary steel producers, color-coded by grade and heat number with automatic band saws.
Ultrasonic degreasing, manganese phosphating, hot-dip galvanizing, laser dot-peen part marking, protective plastic thread caps, and custom seaworthy palletized crating.
Comprehensive breakdown of in-house forging hammers, machining centers, and inspection apparatus.
| Equipment / Machine Category | Make & Technical Model | Quantity | Capacity / Working Envelope | Primary Operation |
|---|---|---|---|---|
| Pneumatic Drop Forging Hammers | Heavy Industrial Steam/Belt Type | 4 Units | 1,000 kg to 5,000 kg Blow Force | Closed-Die Forging of Fittings & Flanges |
| Friction Screw Forging Presses | High-Energy Forging Presses | 3 Units | 400 Ton & 800 Ton Capacity | Precision Sizing & Flash Trimming |
| Induction Billet Heating Systems | Continuous Optical Pyrometer Heaters | 4 Sets | 100 kW to 350 kW (Up to 1250°C) | Uniform Scale-Free Billet Heating |
| CNC Turning Centers & Lathes | Doosan / Haas Multi-Axis CNC | 24 Units | Dia 10mm to 650mm | Length 1000mm | Precision Boring, Facing, SW Sockets & Threads |
| Vertical Machining Centers (VMC) | Rigid Heavy-Duty 4-Axis VMCs | 6 Units | Table: 1200 x 600mm | BT-50 Spindle | Flange Bolt Hole Drilling & Manifold Milling |
| Continuous Heat Treatment Furnaces | Multi-Zone Gas Fired with PID Data Logger | 2 Lines | 5,000 kg Batch Capacity (1200°C) | Normalizing, Annealing, Quenching & Tempering |
| Optical Emission Spectrometer (OES) | 32-Channel Direct Reading PMI Unit | 2 Units | Full UV / Vis Channel Spectrum Analysis | 100% Chemical Composition & Carbon Audit |
| Computerized UTM Tensile Tester | Hydraulic Servo-Controlled 100-Ton | 1 Unit | 0 - 1000 kN Load Measurement | Yield, Tensile Strength & Elongation Testing |
| Hydrostatic Pressure Test Benches | High-Pressure Automated Hydro Skid | 3 Stations | Up to 10,000 PSI Test Pressure | 100% Leak-Tight Proof Pressure Verification |
Rigid quality governance at every step from prime raw billet to finished export crate.
Mill certified prime round bars undergo 100% PMI spectro chemical testing before automatic precision band saw cutting to specific billet weights.
Billets are heated under optical pyrometer monitoring and forged under heavy drop hammers to achieve unbroken metallurgical grain flow.
Components undergo calibrated Normalizing, Solution Annealing, or Q&T to relieve residual stress and achieve specified yield and tensile strength.
Multi-axis CNC turning machines cut micron-accurate socket counterbores and NPT/BSPT threads, followed by ultrasonic, MPI, and dimension audits.
Click any facility image to enlarge in high resolution and examine our production bays.